Stone Composite Floor has moved from a specialist product into a serious option for residential, commercial, and hospitality projects. Its rigid core, water resistance, and realistic wood or stone finishes suit busy spaces, from hotel corridors to family kitchens. Grand View Research valued the global luxury vinyl tiles market at approximately USD 23.9 billion in 2022 and forecasts a 7.7% compound annual growth rate from 2023 to 2030. Stone composite products form part of this wider resilient-flooring movement, although market reports do not always separate SPC from other vinyl categories. That limitation matters.
This guide examines ten Stone Composite Floor options for global buyers. The comparison considers core density, wear-layer thickness, dimensional stability, slip resistance, installation method, warranty terms, and environmental documentation. A beautiful plank can still fail beside a sunny window if its locking system is weak. Installation quality matters, too. Flooring industry analyst Kemp Harr has stated, “The flooring business is a people business,” a useful reminder that supplier communication, technical support, and after-sales service influence real project outcomes. Buyers should request test reports, product samples, batch information, and clear declarations of installation conditions. Certifications can help, but they are not interchangeable. Look closely.
The ranking is practical, not absolute. Climate, subfloor moisture, traffic levels, and local standards can change the best choice. Some options may appear less impressive in photographs yet perform better under rolling chairs, wet footwear, or strong afternoon heat. That is the imperfect part of flooring selection. Product claims deserve verification.
Stone composite flooring combines mineral filler with a polymer binder to create a dense, rigid surface. A typical core contains finely ground limestone and PVC or another engineered resin. The mineral improves stiffness and reduces movement during temperature changes. The resin helps control moisture absorption and supports dimensional stability. Structure matters.
Above the core, a printed film creates wood, stone, or concrete patterns. A transparent wear layer protects the image from daily abrasion. Some constructions include attached acoustic foam underneath. In occupied rooms, this layer can reduce footfall noise and hide minor subfloor irregularities. It cannot correct an uneven base. Poor preparation still shows.
During installation checks, installers should inspect locking edges, cut samples, and expansion gaps. A thicker floor is not automatically stronger. Wear-layer thickness, core density, surface texture, and joint accuracy also affect performance. Stone content alone does not prove quality. Samples can mislead. Global buyers should request test data for dimensional stability, slip resistance, abrasion, and indoor emissions. Test methods differ by market, so comparable laboratory conditions matter. Keep spare planks from the same production batch. Color and texture may change slightly between batches, even when specifications appear identical. That small inconsistency deserves attention.
Stone composite floors should be evaluated against local conditions, not attractive samples alone. A coastal hotel may need strong moisture resistance, while a dry inland home may prioritize thermal comfort. Check water absorption, dimensional stability, surface wear, and slip resistance through independent test reports. Ask whether testing followed standards accepted in the target market.
Climate changes installation requirements. In regions with sharp temperature swings, expansion gaps and subfloor preparation deserve careful review. For humid markets, inspect packaging, warehouse protection, and edge sealing. A damaged carton can hide swollen boards or chipped locking profiles. Request installation instructions in the local language, with clear guidance for concrete, plywood, and radiant heating systems.
Regulations also differ between markets. Verify fire performance, indoor emissions, recycling claims, and product labeling before placing a large order. A specification sheet is useful, but it may not reveal how the floor behaves after months of cleaning and foot traffic. Request production samples from different batches. Compare color, thickness, click fit, and surface texture under natural light.
Small details matter. Very much. Export buyers should also examine lead times, replacement boards, pallet strength, and after-sales technical support. The lowest price can create higher costs through breakage, unsuitable accessories, or installation delays. Some evaluations remain imperfect because laboratory results cannot fully reproduce local buildings. Record those uncertainties instead of hiding them. A reliable supplier should answer difficult questions with evidence, not vague assurances.
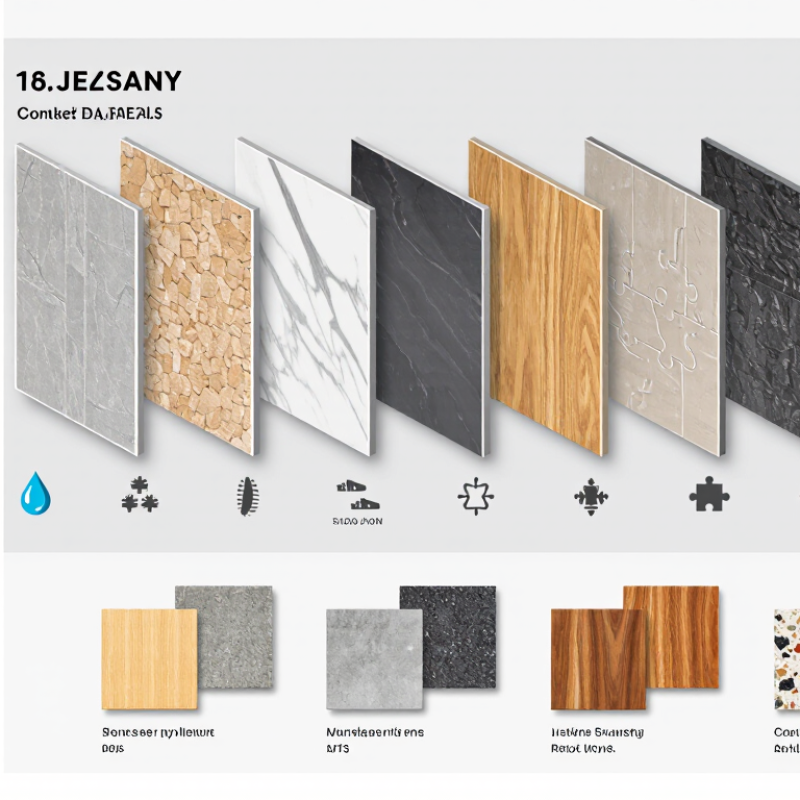
Limestone composite suits calm living rooms and boutique hotels. Marble composite adds a polished appearance to reception areas and dining spaces. Quartz composite offers strong wear resistance in busy corridors. Slate composite works well in entryways, kitchens, and covered outdoor areas. Granite composite handles demanding commercial floors.
Travertine composite creates a softer, natural texture for bedrooms and restaurants. Terrazzo composite supports creative patterns in schools and offices. Concrete-look composite fits modern retail and industrial interiors. Ceramic-stone composite balances easy cleaning with a mineral appearance. Recycled-stone composite may suit sustainability-focused projects, although its color consistency can vary.
The best choice depends on traffic, moisture, subfloor quality, and local installation skills. Rigid mineral-core panels can reduce movement over stable surfaces. They still need expansion gaps. Textured finishes improve underfoot grip, but they may require more cleaning. In my experience, samples under daylight reveal differences that online images hide. A slightly uneven pattern can look more authentic. It can also disappoint highly uniform commercial buyers.
Tips: Request technical sheets, abrasion ratings, slip data, and formaldehyde information. Check thickness, locking tolerance, and carton protection before shipping. Acclimate the flooring when required by the installation guide. Test one small area first. It saves trouble later. Avoid choosing only by price; weak cores, poor edges, and inconsistent printing can increase total project costs.
For global buyers, the ten strongest stone-composite floor options include standard SPC, reinforced SPC, WPC, mineral-core, quartz-polymer, terrazzo composite, recycled stone-polymer, acoustic-core, click-lock, and glue-down systems. Grand View Research valued the global luxury vinyl flooring market at approximately US$40 billion in 2023. That growth reflects demand for rigid, water-resistant surfaces, not automatic quality.
Durability depends on the wear layer, core density, locking profile, and subfloor preparation. ASTM F3261 testing helps evaluate rigid polymer flooring performance. A dense SPC plank suits busy corridors and retail spaces. WPC feels warmer underfoot, but may compress more easily beneath heavy cabinets. Stone-patterned surfaces now imitate veining convincingly. Large-format panels reduce grout lines, although they can expose uneven subfloors. I have seen excellent products fail after rushed installation.
Installation conditions matter across climates. Leave expansion gaps around walls, islands, and door frames. Moisture testing remains essential over concrete slabs. Glue-down systems can manage commercial traffic well, while click-lock products usually reduce labor time.
However, floating floors may sound hollow without suitable acoustic underlay. The European Commission’s Product Environmental Footprint guidance also encourages buyers to examine lifecycle impacts, not only purchase price.
Maintenance is usually simple: remove grit with a soft vacuum, wipe spills quickly, and avoid abrasive pads. Neutral cleaners protect printed surfaces and protective coatings. Some products tolerate damp mopping, but none welcomes standing water. Request independent VOC documentation, such as testing aligned with CDPH Standard Method v1.2. Specifications still vary between batches, so samples should face sunlight, moisture, and rolling loads before approval.
For global buyers, the best stone composite floor depends on market requirements. SPC and mineral-core products differ in density, locking systems, and thermal movement. Request technical sheets before comparing prices. Check slip resistance, fire performance, VOC emissions, formaldehyde levels, and dimensional stability. Requirements vary by country. A test report from one market may not satisfy another. Confirm the testing laboratory, report date, and product reference.
Supplier assessment needs more than attractive samples. Ask about production capacity, core composition, wear-layer thickness, and quality-control records. Request samples from several batches, not one carton. Shade and texture can shift slightly between production runs. That detail is easy to miss. Factory audits, clear tolerances, and written claims procedures improve reliability. A supplier that answers slowly may create larger problems after payment.
Shipping changes the real purchase price. Confirm carton dimensions, pallet limits, container loading plans, moisture protection, and packaging strength. A damaged corner can affect an entire installation. Compare FOB, CIF, and delivered costs carefully. Include freight, insurance, customs duties, port handling, inland transport, and installation waste. Add spare cartons for future repairs. The lowest quotation is not always economical. I have seen buyers overlook local unloading fees and pay more than expected. Recheck every assumption before approving the order.
„Thanks to the LUVIR technology, the solder resist process could be switched directly from the previously used mask exposure to direct exposure. As an outstanding digital solution on the market, this technology has been able to demonstrate fast process times and superior quality on our certified conventional ink in production. This allowed us to fully digitize the solder mask process at low cost – without process or ink adjustments. An excellent benefit to our production in Rot am See.“
Ralf Göhringer (Head of Production WE Rot am See)
I would definitely recommend the Limata machine and team for a future company purchase
Michael Greenaway
Compunetics Inc.
“The Limata ldi has been amazing!! Best thing we did was buy this machine”
Richard Brady
GM
Circuitlabs
“Since 2019, we have been running the Limata X1000 LDI system (including LUVIR for solder mask imaging) in daily production as an addition to our current process with film. The machine was capable of properly exposing Taiyo PSR-4000 BN (DI) solder mask types on normal to high-copper boards using a new and unique direct imaging process. The machine operating interface is very user friendly which allowed for a quick technical training curve. The pre-registration processing reduced several seconds of production time at every print. Limata support and service staff is incomparable. They supported our team every step of the way at basically any time of the day or night, with literally, an immediate response time, customizing the software interface to best fit our Operations and needs.
We have exposed more than 8,000 prints since end of October, on various solder mask colors and some resist film panels. Limata, has proven to be very capable and innovative. They are a strong contender in the industry.
We have very much enjoyed this project, and working with the team!
Thank you Limata for the continued support and being a part of our growth.”
Bill Sezate
Vice President, GM
Summit Interconnect
As a replacement to our current contact exposure process with film, the LIMATA X2000 system including LUVIR-Technology was capable of properly exposing non-LDI solder mask types using a direct imaging process. The machine offers cutting edge software with a very intuitive operating interface which allowed for quick technician training curve. The dual drawer system combined with pre-registration processing reduced several seconds of production time at every machine cycle. Limata support and service staff is world class. They added software patches to keep production running at shortest possible response times, customized the software interface to best fit our in-house Operations system, and even wrote a step-by-step machine processing manual. As a result of the project, we have exposed more than 16,000 times on various product types and solder mask brands/colors. Limata, in a very short timeframe as a company, has definitely shown they are truly innovative and will be challenging the industry of direct imaging for the top spot.
Kevin Beattie
Process Engineer
TTM Technologies
Forest Grove Division