Choosing the right Pump Shaft Seal is not a simple catalog exercise. It requires understanding the pump, fluid, pressure, temperature, and shaft speed. A seal that performs well in clean water may fail quickly with abrasive slurry or crystallizing chemicals. Small details matter. A scratched shaft sleeve can create a visible leak within hours.
Robert N. Flitney, author of Seals and Sealing Handbook, puts the purpose clearly: “The primary function of a seal is to prevent leakage.” His statement sounds obvious, yet many selection mistakes begin by treating the seal as an isolated part. The seal faces, elastomers, spring arrangement, and gland design must work together. Installation quality matters just as much. Even the correct seal can fail after dry running, poor alignment, or contaminated flushing fluid.
This guide explains how to compare seal materials, operating limits, and design types. It also considers maintenance access and total operating cost. A cheaper Pump Shaft Seal may demand frequent replacement. That is not always a saving. In real service, conditions rarely remain perfect. Fluid temperature changes. Solids enter the chamber. Operators make occasional mistakes. Therefore, selection should include a practical safety margin, not only the pump’s nameplate data. The process is not flawless, and assumptions deserve review. A reliable choice comes from verified measurements, manufacturer guidance, and evidence from similar applications.
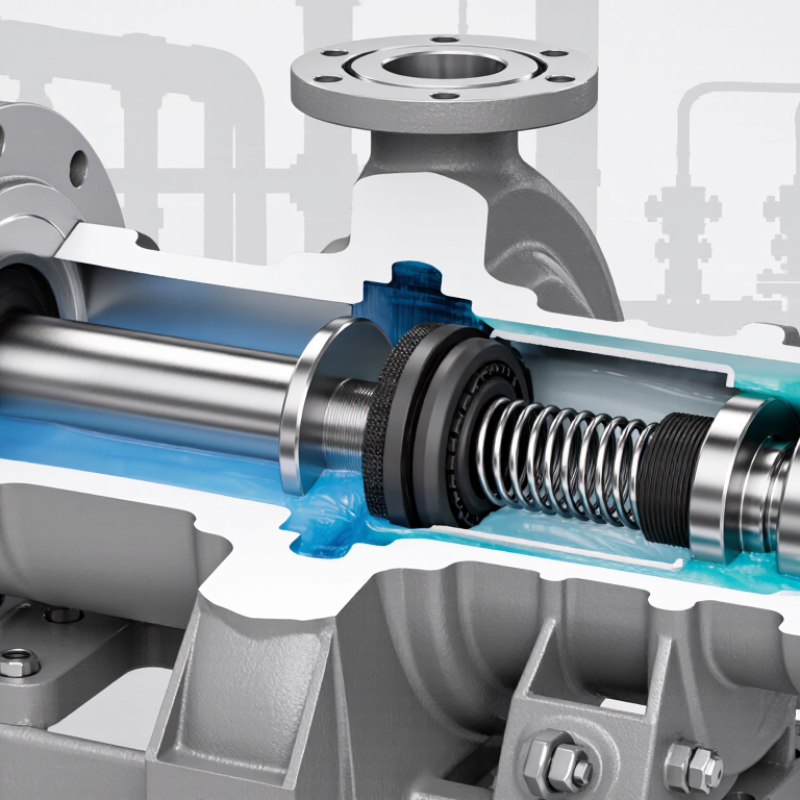
Choosing the right pump shaft seal starts with operating conditions, not catalog dimensions. Record fluid type, temperature, pressure, speed, and shaft size. Note solids, crystallization, viscosity, and whether the pump runs continuously. A clean-water seal may fail quickly with abrasive slurry. Temperature changes matter too. A seal exposed to hot fluid during startup needs suitable materials and cooling. Check alignment, vibration, and shaft runout. These details often reveal the real failure cause.
Seal requirements should match the pump’s actual duty cycle. Select face materials for chemical compatibility and wear resistance. Confirm elastomers tolerate the process fluid and temperature range. Consider single or dual arrangements when leakage control is critical. A dual seal may require a barrier system, monitoring, and trained maintenance. Do not choose by pressure rating alone. Installation quality can matter just as much as seal design. Even experienced teams sometimes overlook dry running during priming.
Tips: Create a simple operating record. Include normal and peak values, startup frequency, flush quality, and previous failure patterns. Ask for compatibility data, dimensional checks, and installation guidance. If conditions are uncertain, test a conservative option under controlled operation. Recheck the choice after the first inspection. The initial selection may not be perfect.
How to Choose the Right Pump Shaft Seal?
Compare the Main Types of Pump Shaft Seals
Choosing a pump shaft seal starts with the liquid, temperature, pressure, and shaft speed. Gland packing is simple, adjustable, and inexpensive. It suits older pumps and liquids that can tolerate slight leakage. However, packing needs regular adjustment and may wear the shaft over time. Mechanical seals normally reduce leakage significantly. They use precisely finished faces, springs, and secondary seals. This design works well for clean liquids and demanding industrial service. Yet, dry running or poor alignment can damage the sealing faces quickly.
Cartridge mechanical seals simplify installation because their components are preassembled. They can reduce fitting errors and maintenance time. Split seals are useful when removing the pump or motor is difficult. Lip seals are compact and practical for low-pressure applications. They are not the best choice for high pressure or abrasive liquids. A common mistake is choosing by pump size alone. Seal materials must also match the fluid. Ceramic, carbon, elastomers, and metal parts each have different limits. Field conditions can be messier than the specification sheet suggests. That is worth checking carefully.
Tips: Confirm shaft diameter, pressure, temperature, speed, and fluid chemistry. Check for solids, crystallization, and dry-start risks. Ask whether controlled leakage is acceptable. Inspect alignment and bearing condition before installation. Even the correct seal can fail on a damaged shaft. If uncertain, compare operating data with the seal maker’s technical guidance.
Mechanical seals generally provide better leakage control than packing, while double mechanical seals are preferred for hazardous, toxic, abrasive, or low-lubricity fluids when a barrier system is available. Lip seals are suitable for lower-pressure applications. The values shown are representative typical limits; actual performance depends on materials, fluid properties, shaft speed, pressure, temperature, and installation quality.
A pump shaft seal should be selected around the fluid, temperature, and pressure—not only the shaft diameter. In field inspections, fluid chemistry often causes failure before normal wear appears. Water may suit carbon and ceramic faces, while abrasive slurry needs harder faces and stronger secondary seals. Choose materials that resist swelling, softening, and chemical attack.
Temperature changes the seal’s behavior quickly. Elastomers can harden in cold service or lose strength near their upper limit. PTFE handles many chemicals, but it may creep under pressure. Graphite tolerates heat well, yet oxidation and fluid compatibility still require checking. The U.S. Department of Energy reports that pumping systems can consume 25–50% of industrial facility electricity. Small leakage can therefore signal both seal loss and wasted energy.
Pressure needs equal attention. Higher pressure increases face loading and can distort softer components. API 682 and ISO 21049 provide useful selection frameworks for mechanical seals, but real operating conditions remain decisive. The NACE IMPACT study estimated global corrosion costs at about $2.5 trillion annually, or 3.4% of global GDP. That figure supports careful material review, especially with saline, acidic, or contaminated fluids. I would record pressure spikes, startup temperature, and dry-running events before final selection. Operators sometimes omit these details. That omission can make a technically correct material choice fail in service.
Check Seal Dimensions, Compatibility, and Installation Needs
Check Seal Dimensions, Compatibility, and Installation Needs
Choosing a pump shaft seal begins with accurate measurements. Check the shaft diameter, seal outside diameter, and installation length. A small error can cause leakage or excessive wear. Measure the shaft with a calibrated micrometer, not a worn ruler. Also inspect the stationary seat and housing bore for scratches or distortion.
Compatibility depends on more than the pumped liquid. Review temperature, pressure, shaft speed, and chemical exposure. The elastomer must tolerate the fluid, while the seal faces must suit its solids and lubrication conditions. For abrasive liquids, face materials need careful evaluation. Ask for verified operating limits when specifications are unclear. Guessing here is expensive.
Installation conditions deserve equal attention. Confirm the seal fits available space and matches the pump’s mounting arrangement. Clean the shaft thoroughly. Remove burrs that could cut the elastomer. Use the recommended lubricant, and protect sealing faces from fingerprints or grit. Never force a spring or twist the rotating face.
I once overlooked a slight shaft groove during inspection; the replacement seal leaked within hours. That mistake changed my checklist. Shaft runout and endplay should be measured before installation, although these checks are often skipped. A smooth shaft does not always mean a true shaft.
How to Choose the Right Pump Shaft Seal?
Evaluate Service Life, Maintenance, Cost, and Support
Choosing a pump shaft seal starts with service life, not purchase price. A seal faces heat, pressure, abrasives, dry running, and chemical attack. During inspections, polished sleeves and brown leakage tracks often reveal unstable operation. Look for patterns. If failures occur every few months, review alignment, flushing, pressure, and material compatibility before selecting a stronger seal.
Lifecycle cost deserves careful attention. The Hydraulic Institute and Europump’s Pump Life Cycle Costs guide indicates that energy may represent about 40% of total pump ownership cost. Maintenance and downtime can add significantly more. The U.S. Department of Energy reports that pumping systems use nearly 20% of industrial motor electricity, with potential savings of 20–50% in suitable systems. A seal that reduces leakage but increases friction may not deliver the expected value. The estimate varies by duty.
Maintenance should be simple enough for technicians to perform correctly. Check installation space, replacement time, spare-part availability, and inspection access. The U.S. Department of Energy’s Operations and Maintenance Best Practices Guide associates effective maintenance with 5–20% energy savings in appropriate facilities. Support also matters. Ask for installation drawings, operating limits, failure-analysis guidance, and response times. A common mistake is treating a low price as proof of value. It is not always. Review real maintenance records, not only catalog claims, and leave room to question your original selection when field evidence disagrees.
General comparison of common pump shaft sealing solutions for water, process fluids, and industrial applications
| Seal Type | Typical Service Life | Maintenance Requirement | Initial Cost | Typical Operating Conditions | Leakage Control | Installation Complexity | Support and Spare-Part Considerations | Best-Fit Applications |
|---|---|---|---|---|---|---|---|---|
| Packed Gland Seal | Approximately 3–12 months, depending on shaft condition, adjustment, fluid abrasiveness, and operating hours | High Requires regular packing adjustment and periodic replacement | Low | Low to moderate pressure; commonly used for water and less hazardous fluids | Controlled leakage is normally required for cooling and lubrication | Low; packing can usually be replaced without removing the pump | Generally easy to source; correct packing size, material, and installation technique are important | Basic water service, slurry duties, older equipment, and applications where limited leakage is acceptable |
| Single Mechanical Seal | Approximately 1–3 years under suitable conditions; shorter life may occur with dry running, vibration, or solids | Medium Requires correct installation, clean faces, and periodic condition checks | Medium | Moderate pressure and temperature; compatible with many clean or lightly contaminated liquids | Very low visible leakage when properly selected and operated | Medium; shaft runout, alignment, face condition, and elastomer compatibility matter | Replacement parts should match seal dimensions, face materials, elastomers, and spring arrangement | General industrial pumps, cooling water, process water, oils, and non-crystallizing chemicals |
| Cartridge Mechanical Seal | Approximately 2–5 years in stable service with proper flushing and operating conditions | Low to Medium Pre-assembled design reduces setup errors; routine inspection is still required | Medium to High | Moderate to high pressure and temperature, subject to material and design limits | Very low leakage when correctly selected and maintained | Low to medium; preset components simplify installation and alignment | Spare cartridges should be stocked by pump size and seal arrangement; technical fit verification is recommended | Plants seeking faster maintenance, repeatable installation, and reduced assembly-related failures |
| Double Mechanical Seal | Approximately 2–5 years when barrier fluid pressure, cleanliness, and circulation are properly controlled | Medium to High Requires barrier or buffer system checks, pressure monitoring, and fluid management | High | Hazardous, toxic, abrasive, volatile, crystallizing, or difficult-to-seal fluids | Excellent containment; the secondary seal helps prevent process fluid from escaping | High; requires correct piping plan, barrier fluid, pressure setting, and commissioning | Support should include seal selection, piping-plan guidance, spare parts, and troubleshooting assistance | Chemical processing, hydrocarbons, hazardous liquids, high-value fluids, and emissions-sensitive service |
| Split Mechanical Seal | Approximately 1–4 years, depending on shaft condition, installation quality, vibration, and fluid properties | Medium Allows seal replacement without removing large pumps, but installation accuracy is essential | Medium to High | Large-diameter shafts, large pumps, and equipment where dismantling is costly or difficult | Very low leakage when properly fitted and operated | Medium to high; split faces and components require careful cleaning, measurement, and alignment | Availability of correctly sized split components and field installation support can significantly reduce downtime | Large cooling-water pumps, circulating systems, power utilities, and continuous-process equipment |
„Thanks to the LUVIR technology, the solder resist process could be switched directly from the previously used mask exposure to direct exposure. As an outstanding digital solution on the market, this technology has been able to demonstrate fast process times and superior quality on our certified conventional ink in production. This allowed us to fully digitize the solder mask process at low cost – without process or ink adjustments. An excellent benefit to our production in Rot am See.“
Ralf Göhringer (Head of Production WE Rot am See)
I would definitely recommend the Limata machine and team for a future company purchase
Michael Greenaway
Compunetics Inc.
“The Limata ldi has been amazing!! Best thing we did was buy this machine”
Richard Brady
GM
Circuitlabs
“Since 2019, we have been running the Limata X1000 LDI system (including LUVIR for solder mask imaging) in daily production as an addition to our current process with film. The machine was capable of properly exposing Taiyo PSR-4000 BN (DI) solder mask types on normal to high-copper boards using a new and unique direct imaging process. The machine operating interface is very user friendly which allowed for a quick technical training curve. The pre-registration processing reduced several seconds of production time at every print. Limata support and service staff is incomparable. They supported our team every step of the way at basically any time of the day or night, with literally, an immediate response time, customizing the software interface to best fit our Operations and needs.
We have exposed more than 8,000 prints since end of October, on various solder mask colors and some resist film panels. Limata, has proven to be very capable and innovative. They are a strong contender in the industry.
We have very much enjoyed this project, and working with the team!
Thank you Limata for the continued support and being a part of our growth.”
Bill Sezate
Vice President, GM
Summit Interconnect
As a replacement to our current contact exposure process with film, the LIMATA X2000 system including LUVIR-Technology was capable of properly exposing non-LDI solder mask types using a direct imaging process. The machine offers cutting edge software with a very intuitive operating interface which allowed for quick technician training curve. The dual drawer system combined with pre-registration processing reduced several seconds of production time at every machine cycle. Limata support and service staff is world class. They added software patches to keep production running at shortest possible response times, customized the software interface to best fit our in-house Operations system, and even wrote a step-by-step machine processing manual. As a result of the project, we have exposed more than 16,000 times on various product types and solder mask brands/colors. Limata, in a very short timeframe as a company, has definitely shown they are truly innovative and will be challenging the industry of direct imaging for the top spot.
Kevin Beattie
Process Engineer
TTM Technologies
Forest Grove Division