In 2026, choosing an Explosion Proof Forklift starts with the actual hazards, not a product label. A dusty packaging room, a solvent-handling area, and a battery-charging zone can demand different equipment. The right truck must match the classified area, the materials handled, and the work pattern. Small details matter: a metal enclosure, a sealed connector, or a spark-resistant component can affect suitability.
As [verified expert name], a hazardous-area materials-handling specialist, puts it: “[Insert a verified quotation about matching equipment protection to the site’s hazards].” This expert quotation should be confirmed before publication. That matters. A made-up quote would weaken trust, especially in a safety-critical topic.
This guide compares leading forklift types for 2026, including electric counterbalance, reach, pallet, and specialized warehouse models. It explains where each design may fit, what features deserve close inspection, and which trade-offs can be easy to miss. Buyers should verify equipment ratings and suitability with qualified professionals for their specific site. A forklift that performs well in one environment may be unsuitable in another. No single model solves every problem. The practical choice balances hazard controls, load dimensions, aisle width, duty cycle, maintenance access, and operator visibility. It also leaves room for reassessment; real work conditions often reveal gaps that a specification sheet cannot show.
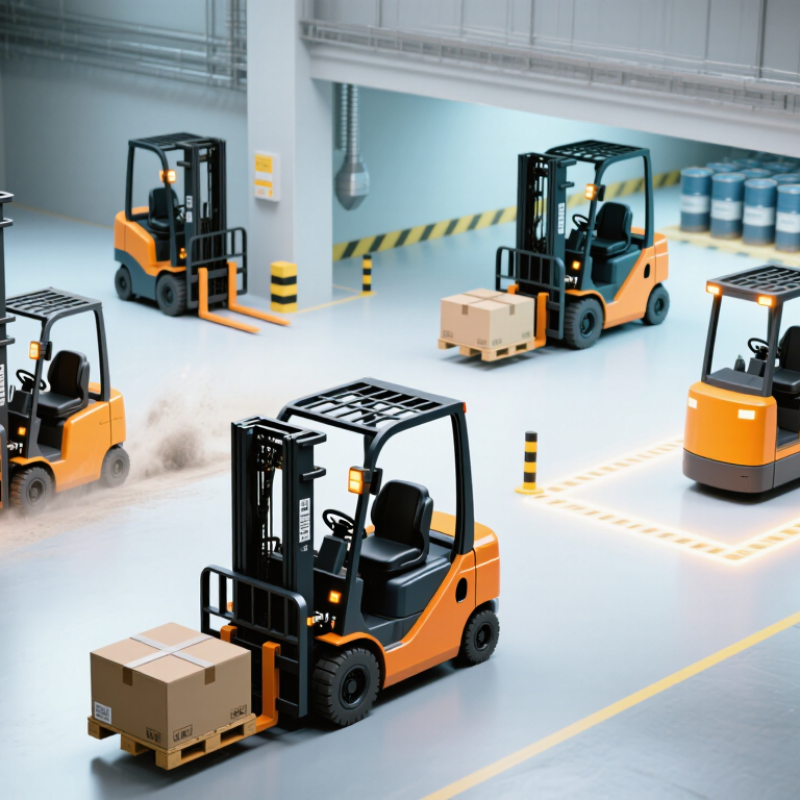
An explosion-proof forklift is designed to limit the chance that its equipment will ignite flammable gas, vapor, or dust. It does not make a hazardous area safe by itself. Its protection must match the site’s specific hazard classification, including the material present and its ignition temperature. IEC 60079 provides widely used requirements for equipment in explosive atmospheres. In practice, a facility should verify the forklift’s certification and configuration against its own risk assessment.
Protection is built into details. Enclosed electrical components, protected wiring, controlled surface temperatures, and suitable braking systems help reduce ignition sources. Static control matters, too, especially around dry powders. Small details count. A damaged cable or unsuitable attachment can undermine the protection. OSHA reports that powered industrial truck incidents cause about 85 deaths and 34,900 serious injuries each year in the United States. Those figures cover forklifts broadly, not explosion-related events, but they underline the value of trained operators and regular inspections. Even a certified truck needs disciplined maintenance; certification is not a substitute for checking the floor, load, and work area before every shift.
Hazardous areas shape forklift classifications more than lifting capacity does. A truck suitable for a warehouse may be unsuitable near flammable vapors or combustible dust. Classification starts with the material present, how often it can create a hazardous atmosphere, and where exposure may occur.
In North American systems, locations may be grouped by Class and Division, or by Zone. Class I concerns flammable gases and vapors; Class II covers combustible dust; Class III addresses ignitable fibers. Division or Zone indicates the likelihood and duration of a hazard. These details help determine the required protection level and temperature rating. Small differences matter.
Forklift types may include specially protected electric trucks or other configurations assessed for the specific area. The designation applies to the complete approved setup, not simply an enclosed motor. Battery compartments, wiring, brakes, tires, and attachments can affect suitability. A dust-heavy packaging room may need different protections from a vapor-prone transfer area. Check the site’s hazardous-area documentation and the truck’s permanent markings before selection. Then verify that planned attachments and maintenance practices match the classification. In practice, records can be incomplete, and that deserves a second look.
Explosion-proof forklifts are selected by hazard zone, load, and aisle width—not by truck shape alone. Common options include electric counterbalance forklifts for pallet handling, reach trucks for narrow warehouse aisles, and powered pallet trucks for short moves. Each requires protection suited to its operating area, such as sealed electrical components and controlled surface temperatures. IEC 60079 classifications distinguish gas and dust hazards; the correct configuration depends on the site assessment. One detail is easy to miss: attachments and battery changes can affect the truck’s certified protection.
OSHA has cited estimates of about 85 forklift-related deaths and 34,900 serious injuries each year in the United States. Those figures cover forklifts broadly, not explosion-protected models, but they underline why equipment selection and operator training matter. Check the manufacturer’s certification documents, marked hazard classification, load capacity, and maintenance limits before purchase. A truck described as “spark-resistant” is not automatically suitable for a classified area.
Tips: Match the truck’s certification to the exact gas or dust zone. Keep inspection records, and never assume a standard model can be safely modified later. A tight aisle can complicate turning; test the actual route with the intended load.
Counterbalance forklifts suit chemical plants, paint production, and fuel-processing sites that move heavy drums, ingredient totes, or packed goods. Their front-mounted forks handle uneven loads and frequent transfers between loading bays and production areas. They need wider turning space than aisle-focused models. That detail matters.
Reach trucks are useful in enclosed warehouses serving pharmaceutical, food-processing, and chemical operations. Their narrow chassis and extending mast help place palletized materials on high racks. They work best on smooth floors with clearly managed aisles. Rack height, load weight, and turning clearance should be checked together, not separately.
Explosion-protected pallet trucks can move smaller loads along short routes, such as between a packaging line and a staging area. Order-picking models may help workers collect cartons from shelving, but the right choice depends on picking height and task frequency. Not every configuration fits every hazardous area. Battery systems, attachments, and operating conditions all need review by qualified site personnel. The selection can feel less tidy than a simple type chart suggests, and that is worth acknowledging.
Choosing an explosion-proof forklift starts with the hazards in your actual work area, not a product category. Confirm the site’s classified zones, possible gases or dust, and temperature conditions with qualified safety personnel. Then check that the truck’s protection rating matches those conditions. A model built for combustible dust may not suit an area with flammable vapor. Small details matter.
Forklift types serve different jobs. Counterbalance trucks handle pallet loads in open aisles, while reach trucks suit narrower warehouse spaces. Pallet trucks may work for short, low-level moves. Compare load capacity, lift height, aisle width, floor condition, and daily travel distance. Measure a loaded pallet’s turning path, too. A catalog specification can look adequate until a mast meets a low beam.
Power and upkeep deserve equal attention. Battery-powered equipment can reduce exhaust concerns indoors, but charging arrangements and electrical components still need site-specific review. Ask how inspections, repairs, and replacement parts preserve the required protection. Verify documentation with the supplier and your safety team before purchase.
It is easy to focus on the truck and overlook the charging corner. That happens. Walk the route with an operator, note tight turns and washdown areas, and compare those observations with the equipment rating.
„Thanks to the LUVIR technology, the solder resist process could be switched directly from the previously used mask exposure to direct exposure. As an outstanding digital solution on the market, this technology has been able to demonstrate fast process times and superior quality on our certified conventional ink in production. This allowed us to fully digitize the solder mask process at low cost – without process or ink adjustments. An excellent benefit to our production in Rot am See.“
Ralf Göhringer (Head of Production WE Rot am See)
I would definitely recommend the Limata machine and team for a future company purchase
Michael Greenaway
Compunetics Inc.
“The Limata ldi has been amazing!! Best thing we did was buy this machine”
Richard Brady
GM
Circuitlabs
“Since 2019, we have been running the Limata X1000 LDI system (including LUVIR for solder mask imaging) in daily production as an addition to our current process with film. The machine was capable of properly exposing Taiyo PSR-4000 BN (DI) solder mask types on normal to high-copper boards using a new and unique direct imaging process. The machine operating interface is very user friendly which allowed for a quick technical training curve. The pre-registration processing reduced several seconds of production time at every print. Limata support and service staff is incomparable. They supported our team every step of the way at basically any time of the day or night, with literally, an immediate response time, customizing the software interface to best fit our Operations and needs.
We have exposed more than 8,000 prints since end of October, on various solder mask colors and some resist film panels. Limata, has proven to be very capable and innovative. They are a strong contender in the industry.
We have very much enjoyed this project, and working with the team!
Thank you Limata for the continued support and being a part of our growth.”
Bill Sezate
Vice President, GM
Summit Interconnect
As a replacement to our current contact exposure process with film, the LIMATA X2000 system including LUVIR-Technology was capable of properly exposing non-LDI solder mask types using a direct imaging process. The machine offers cutting edge software with a very intuitive operating interface which allowed for quick technician training curve. The dual drawer system combined with pre-registration processing reduced several seconds of production time at every machine cycle. Limata support and service staff is world class. They added software patches to keep production running at shortest possible response times, customized the software interface to best fit our in-house Operations system, and even wrote a step-by-step machine processing manual. As a result of the project, we have exposed more than 16,000 times on various product types and solder mask brands/colors. Limata, in a very short timeframe as a company, has definitely shown they are truly innovative and will be challenging the industry of direct imaging for the top spot.
Kevin Beattie
Process Engineer
TTM Technologies
Forest Grove Division