In practical packaging work, material choice affects protection, efficiency, and customer trust. Foil Roll remains a strong option for products facing moisture, oxygen, light, or temperature changes. Its reflective surface can help reduce heat exposure during storage and transport. Its compact form also supports high-speed converting and customized package sizes.
The right structure depends on the product. Pharmaceutical applications may require controlled thickness, clean surfaces, and verified barrier performance. Food manufacturers often examine seal strength, pinholes, migration data, and printing quality. Industrial users may prioritize durability, flexibility, and resistance to chemicals. These decisions should follow documented testing, not attractive claims. A qualified supplier should provide technical data, traceability, and consistent batch control.
Global packaging needs also demand careful attention to regional standards and recycling systems. Foil can protect products with very little material, yet its recovery depends on the final package design. Thin foil laminates may perform well but can be difficult to separate. That limitation deserves honest discussion. No material solves every packaging problem. Not by itself.
A reliable selection process compares barrier requirements, forming behavior, sealing conditions, logistics, and total cost. It also considers production waste and the customer’s disposal environment. Experienced teams should test samples under realistic humidity, pressure, and transport conditions. Small defects can become expensive failures. Foil Roll is valuable when its technical strengths match the application, the supplier is accountable, and performance is measured from production line to end use.
Why Choose Foil Roll for Global Packaging Needs?
What Foil Roll Is and How It Functions in Packaging
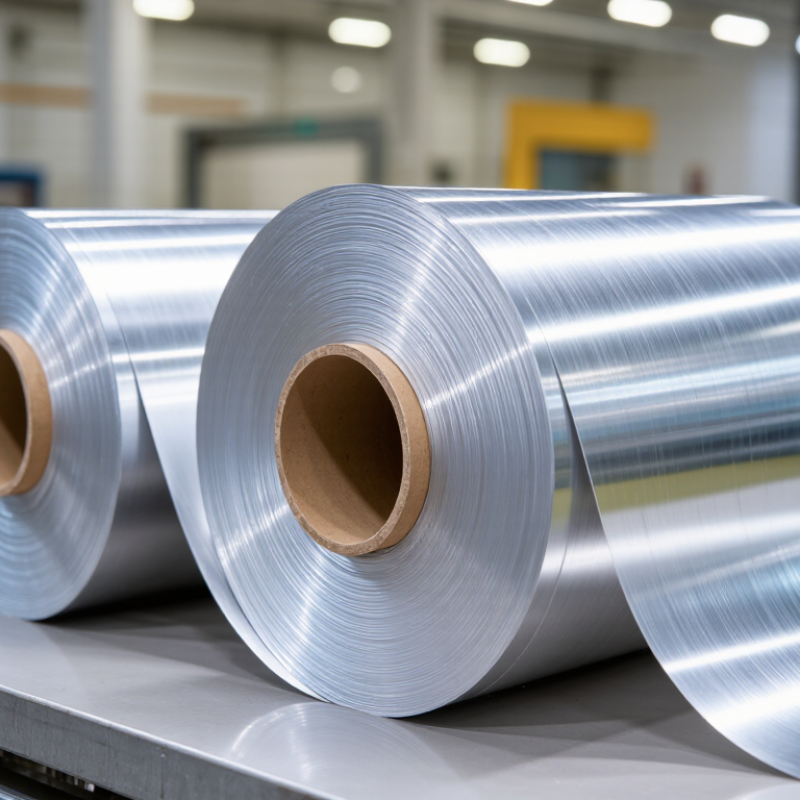
Foil roll is a continuous sheet of aluminium supplied in large industrial coils. Converters slit, laminate, print, or form it for different packaging structures. Its main function is barrier protection. The metal blocks light, oxygen, moisture, and many aromas. This helps protect sensitive products during storage and transport.
Thickness matters. A thinner foil can reduce material use, but it may tear during converting or filling. A thicker grade offers better puncture resistance, although it adds weight and cost. In practical packaging trials, weak seals often cause more failures than the foil itself. That detail is easy to overlook. The International Aluminium Institute reports that recycling aluminium uses roughly 5% of the energy required for primary production. However, laminated foil structures can be difficult to separate and recycle. Design decisions should consider the full package, not only the foil layer.
Tips: Specify the required barrier level before selecting thickness. Test rolls under actual humidity, temperature, and filling conditions. Check edge quality, winding tension, and seal compatibility. The FAO estimates that 14% of food is lost between harvest and retail, so reliable barrier packaging can support waste reduction. Still, foil is not automatically the best choice. Engineers should compare protection, recyclability, machine performance, and total material use.
Why Choose Foil Roll for Global Packaging Needs?
Key Barrier Properties That Protect Packaged Products
Foil roll helps protect products from moisture, oxygen, light, and unwanted odors. These barriers matter during long storage and international transport. A dry food product may lose texture when humidity enters the package. Light can also reduce color, flavor, and nutrient quality. Foil’s near-total light barrier offers dependable protection in warehouses, trucks, and retail displays. Its low oxygen transmission helps slow oxidation. This supports fresher taste and more stable product quality.
In packaging trials, seal performance often matters as much as foil thickness. Tiny pinholes, edge damage, or flex cracks can weaken protection. A suitable foil structure should match the product, filling process, and climate. Humid routes need strong moisture resistance. Products with strong aromas require reliable odor retention. Testing oxygen transmission, water vapor transmission, seal strength, and pinhole resistance improves confidence. Still, thicker foil is not automatically better. It may increase material use without solving a weak seal.
Tips: Check the full package structure, not foil alone. Review barrier test results before production. Inspect rolls for creases, dust, and edge damage. Keep storage areas clean and dry. Small defects matter.
Aluminum foil laminates provide the strongest oxygen barrier among common flexible packaging structures. The lower the oxygen transmission rate, the better the protection against oxidation, aroma loss, and product degradation. Values shown are representative industry ranges and may vary with material grade, thickness, coating, sealing quality, and package design.
Foil roll plays a practical role in packaging that must resist light, oxygen, moisture, and temperature changes. In food packaging, manufacturers use it for coffee, baked goods, dairy portions, snacks, and ready-to-eat meals. Its barrier layer helps preserve aroma and texture during storage and transport. Converters can adjust thickness, coating, and sealing methods for different product shapes.
Small details matter. Seal strength, pinholes, and roll tension require regular inspection.
Pharmaceutical packaging uses foil roll for blister lidding, sachets, and unit-dose packs. These formats help protect tablets and powders from humidity and contamination.
Clear printing and batch information also support traceability. In personal care, foil-based laminates protect creams, gels, masks, and single-use samples. Medical packaging may require clean surfaces, controlled production areas, and documented testing.
Requirements vary across markets, so one specification cannot serve every region.
Electronics and industrial manufacturers also use foil roll for moisture-sensitive components, protective pouches, insulation layers, and chemical-resistant packaging. These applications often demand precise dimensions and stable sealing performance.
However, foil is not automatically the best choice. Multilayer structures can complicate recycling, and poor storage may cause creases or oxidation. That assumption deserves review.
Reliable suppliers should provide material data, production records, and test results that match the intended application. Practical trials remain essential, especially when packaging moves through humid warehouses, long shipping routes, or repeated temperature changes.
Foil roll supports global packaging when safety evidence travels with the material. Its barrier blocks light, oxygen, moisture, and many contaminants. That protection can extend shelf life and reduce avoidable food waste. Food-contact compliance still requires documented testing, not assumptions. In Europe, Regulation (EC) No. 1935/2004 requires materials to avoid harmful migration. In the United States, applicable food-contact requirements and migration testing guide market access. Do not rely on appearance alone. A clean surface proves little.
Tips: Request migration reports, alloy details, and coating specifications. Confirm temperature limits for filling, cooking, and storage. Record supplier lots and inspection results. Ask whether local recyclers accept household foil. The International Aluminium Institute reports that recycling aluminium can save up to 95% of primary-production energy. However, thin foil often escapes collection when food residue remains. A recyclable material is not always recycled. UNEP’s Global Waste Management Outlook 2024 projects municipal waste could rise from 2.3 billion tonnes in 2023 to 3.8 billion tonnes by 2050.
Export teams should check destination rules for packaging composition, labeling, and producer responsibility. Requirements can differ between neighboring markets. The EU increasingly emphasizes recyclability and packaging reduction. Several other jurisdictions use separate recovery targets. Foil laminates may improve performance, yet mixed layers can complicate recycling. That trade-off deserves honest review. In practice, the best specification balances barrier performance, verified safety, transport conditions, and realistic local recovery.
Selecting the right foil roll begins with the product, not the supplier’s catalog. Define the required thickness, width, alloy, temper, and surface finish. These details affect forming performance, barrier protection, and production speed. A thin roll may reduce material use. However, it can tear during high-speed filling. A thicker grade may improve strength but increase shipping weight. The balance matters.
Global supply chains add practical concerns. Confirm the roll’s core diameter and maximum outer diameter before ordering. A small mismatch can stop an otherwise prepared line. Check flatness, edge quality, winding tension, and splice control. Request measurable tolerances, inspection records, and a sample roll when possible. Packaging should protect the foil from moisture, dust, and crushed edges. Use sealed wrapping and stable pallets. Humidity is easy to underestimate.
Do not judge quality by appearance alone. Test thickness across several points, examine pinholes, and review batch consistency. Ask whether production documents support the destination market’s packaging requirements. Requirements can differ by region and application. Lead time also needs a buffer for transport delays and port handling. I once overlooked storage space when comparing roll sizes. The price looked efficient, but the warehouse could not handle the shipment smoothly. That mistake changed my checklist. Good selection is not only technical. It must fit equipment, storage, documentation, and real delivery conditions.
„Thanks to the LUVIR technology, the solder resist process could be switched directly from the previously used mask exposure to direct exposure. As an outstanding digital solution on the market, this technology has been able to demonstrate fast process times and superior quality on our certified conventional ink in production. This allowed us to fully digitize the solder mask process at low cost – without process or ink adjustments. An excellent benefit to our production in Rot am See.“
Ralf Göhringer (Head of Production WE Rot am See)
I would definitely recommend the Limata machine and team for a future company purchase
Michael Greenaway
Compunetics Inc.
“The Limata ldi has been amazing!! Best thing we did was buy this machine”
Richard Brady
GM
Circuitlabs
“Since 2019, we have been running the Limata X1000 LDI system (including LUVIR for solder mask imaging) in daily production as an addition to our current process with film. The machine was capable of properly exposing Taiyo PSR-4000 BN (DI) solder mask types on normal to high-copper boards using a new and unique direct imaging process. The machine operating interface is very user friendly which allowed for a quick technical training curve. The pre-registration processing reduced several seconds of production time at every print. Limata support and service staff is incomparable. They supported our team every step of the way at basically any time of the day or night, with literally, an immediate response time, customizing the software interface to best fit our Operations and needs.
We have exposed more than 8,000 prints since end of October, on various solder mask colors and some resist film panels. Limata, has proven to be very capable and innovative. They are a strong contender in the industry.
We have very much enjoyed this project, and working with the team!
Thank you Limata for the continued support and being a part of our growth.”
Bill Sezate
Vice President, GM
Summit Interconnect
As a replacement to our current contact exposure process with film, the LIMATA X2000 system including LUVIR-Technology was capable of properly exposing non-LDI solder mask types using a direct imaging process. The machine offers cutting edge software with a very intuitive operating interface which allowed for quick technician training curve. The dual drawer system combined with pre-registration processing reduced several seconds of production time at every machine cycle. Limata support and service staff is world class. They added software patches to keep production running at shortest possible response times, customized the software interface to best fit our in-house Operations system, and even wrote a step-by-step machine processing manual. As a result of the project, we have exposed more than 16,000 times on various product types and solder mask brands/colors. Limata, in a very short timeframe as a company, has definitely shown they are truly innovative and will be challenging the industry of direct imaging for the top spot.
Kevin Beattie
Process Engineer
TTM Technologies
Forest Grove Division